Problem statement: suppliers look fine on paper but fail in process
Surface claims like “low-odor” or “high-stability” rarely predict factory performance. You’re facing melt-index drift, dispersion blind spots, and unexpected downstream defects — not marketing copy. Start by treating any additive catalog entry as a hypothesis: confirm Tg shifts, MFI impacts, and thermal stability before you commit. If you want to validate formulations fast, run targeted trials with the specific resin and processing window rather than rely on blanket specs for plastic additives.
Real-world anchor: supplier vetting from trade shows to sourcing hubs
After benchmarking compounds at the K Fair in Düsseldorf and audits in Guangdong, I observed repeat patterns: inconsistent concentrate homogeneity, incomplete SDS updates, and weak lab-to-line correlation. Those meetings taught a simple rule — verify technical service depth and traceability when you evaluate plastic additives suppliers. A supplier who brings repeatable lab protocols and batch-level documentation reduces scale-up risk.
Technical checks you must run
Run DSC and TGA for thermal transitions and degradation onset; measure MFI (or melt flow rate) pre- and post-additive at target dosing; use dynamic rheometry to detect shear-thinning or thickening that will alter die pressure. Check particle size distribution for powders and dispersion index for concentrates. Confirm additive volatility under your extrusion or injection cycle — a 10–20°C difference in residence temperature can change chemistry outcomes dramatically.
Compatibility and formulation physics
Compatibility isn’t vague. Match polarity: nonpolar base polymers (PP, PE) need nonpolar carriers or proper compatibilizers; polar resins (PC, PA, PET) often require coupling agents or reactive additives. Watch for antagonistic interactions — certain antioxidants can inhibit flame retardants or cause color shifts when combined with nucleating agents. Use small-scale compounding trials with incremental dosing to map response curves rather than single-point tests.
Processing considerations that break or make production
Shear and temperature matter. High-shear extrusion can shear-stress sensitive additives, creating plate-out or filter blocking. Additives with low thermal stability should be dosed via side-feed or masterbatch at lower melt temperatures. Check residence-time distribution for your screw design; long tail RTD magnifies degradation. Validate downstream operations — thermoforming, printing, or metallization — since additive residue or surface energy changes alter adhesion and coating behavior.
Lab-to-line correlation: protocols that prove supplier claims
Demand a supplier-provided verification protocol: recommended lab conditions, sample compounding recipe, acceptance thresholds for dispersion (e.g., ppm of agglomerates), and target mechanical/end-use tests. Run scaled trials: bench compounder → pilot extruder → production line. Track at least three metrics across scales: melt torque, die pressure, and visual defect rate. If those diverge, flag the additive for reformulation or alternative dosing strategy.
Common pitfalls and how to avoid them
Assuming “works with all resins” is the top trap. Not planning for storage and handling (hygroscopic additives, UV stabilizers losing efficacy when exposed) is another. Avoid single-source dependency without backup grades; resins and additives both face supply shocks. Don’t skip shelf-life testing; some concentrates lose dispersibility after shipping stress. Lastly, underestimating needed technical support — an additive is a tool, but the supplier’s troubleshooting capability is the real asset.
Decision checklist for supplier selection
Confirm: batch-level COA and traceability, on-site or remote technical support with process engineers, pilot trial data using your resin and machinery, clear SDS and regulatory compliance for target markets, and contingency grades for supply interruptions. Price matters, but quantify cost-per-defect reduction and process stability gains when you compare bids. Prefer suppliers who provide defined dispersion protocols and measurable acceptance criteria.
Conclusion: practical outcome and pathway forward
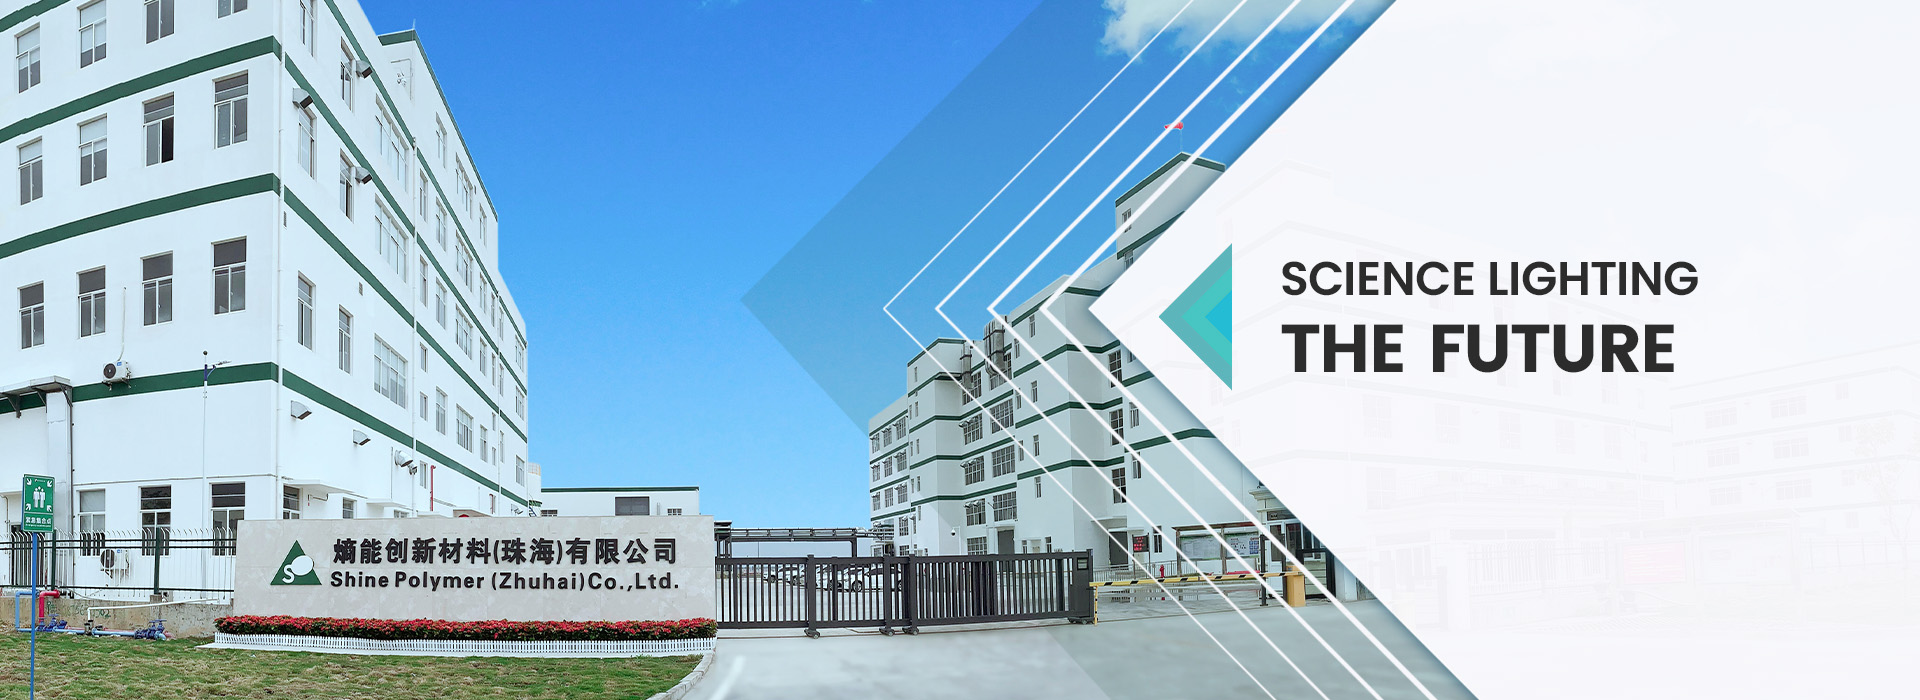
You need fewer surprises and more predictable runs. Use targeted analytics (DSC, TGA, rheology), insist on lab-to-line validation, and pick partners who supply data and troubleshooting — not just product sheets. That combination of technical rigor and operational support is what makes procurement a strategic advantage rather than a recurring risk, and it’s the pragmatic value Shine Polymer brings to the table: tested specs, traceability, and on-line problem-solving that align with production realities Shine Polymer.
