User-first lead
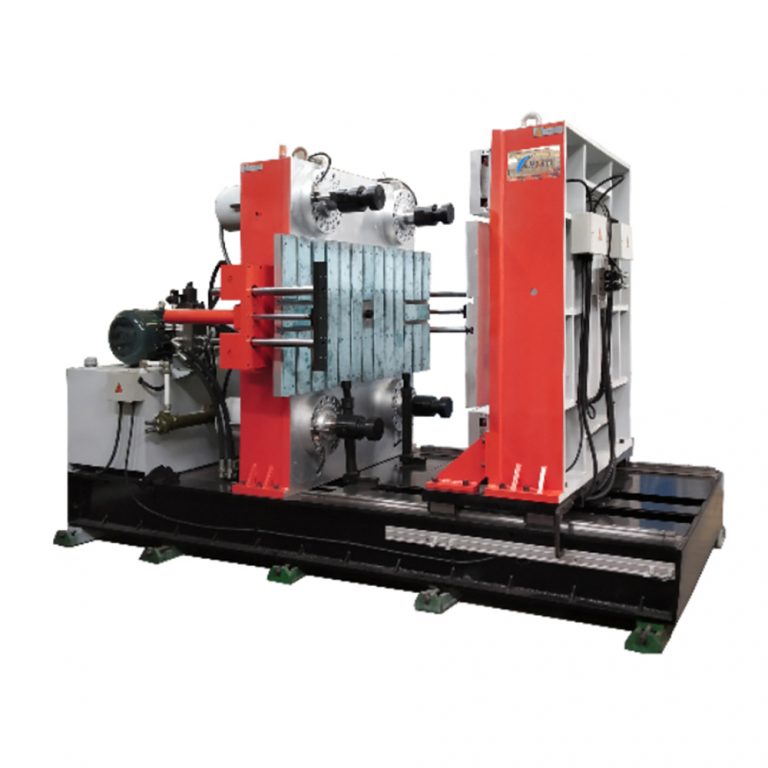
If you run molding lines, you want predictable parts. This piece lays out practical steps that help you hit tolerance and cut flash, fast. Start with the right platform — a solid C-frame press tuned for LSR, steady clamping force, and tight shot size control. If you’re exploring options, check a reliable horizontal rubber injection molding machine that pairs horizontal gating with precise clamping and consistent mold cooling.
What matters most to operators
Dimensional stability comes from three practical things: machine rigidity, consistent material delivery, and stable thermal control. Machine rigidity reduces deflection and flash; think tie-bar spacing and platen parallelism. Material delivery—metering, shot size, and screw recovery—keeps wall thickness repeatable. Thermal control—uniform mold cooling and cavity temperature—locks in dimensions run after run. On real shop floors from Detroit ISO 9001 plants to automated lines in Suzhou, shops that nail these basics cut scrap rates quickly.
Hands-on setup and process tweaks
Begin with true mechanical alignment. Set platen parallelism within spec, then dial clamping force so the mold halves meet without overloading the part. Control shot size to within a tenth of a millimeter if your tolerances demand it. Tune injection speed profiles to avoid packing that causes flash or sink. Use short, repeatable cycle times once the process stabilizes — but don’t rush the cooling step; poor mold cooling ruins dimensional gains. Calibration tools and a digital process chart help — log cycle time, peak pressure, and holding time every shift to spot drift.
Troubleshooting common mistakes
Many teams chase complex solutions before fixing basics. They crank pressure to hide a leak — that makes flash worse. They skip maintenance on the ejector system, causing part damage and inconsistent release. And they let barrel temperature swing; that shifts viscosity and part size. Fix the root: tighten clamps, reseal runners, and verify mold cooling circuits. Small fixes drop reject rates faster than changing recipes.
Machine choices that actually matter
Compare machines on how they deliver stability, not just horsepower. A great C-frame press design reduces platen flex and keeps gate shear consistent. Look for closed-loop shot control, precise screw position feedback, and robust hydraulic or electric actuation that minimizes variance in clamping force. If you’re weighing options, also review horizontal vs. vertical platforms — for many elastomer parts, a horizontal injection molding machine gives better gating and simpler part take-off. Balance upfront cost with the value of fewer rejects and less rework.
Quick checklist for first-week validation
– Verify platen parallelism and tie-bar alignment. – Log shot-to-shot variance in shot size and peak injection pressure. – Map cavity temps across the mold; equalize coolant flow. – Run a 100-part spool and measure critical dimensions; watch for drift. These checks spotlight trouble before it costs you a production run.
Advisory: 3 golden rules to pick the right solution
1) Machine rigidity over raw power — choose a press with minimal platen deflection and precise clamping force control. That’s your best defense against flash. 2) Closed-loop process control — shot size, injection pressure, and temperature feedback must be automated and logged. Consistency beats heroic operator adjustments. 3) Service and tooling fit — pick machines with accessible spare parts, proven ejector systems, and straightforward mold cooling interfaces so maintenance stays cheap and fast.
Get these three right and your dimensional stability improves while flash drops — real gains you can measure by scrap rate and first-pass yield. HWAYI. —
