User-first overview
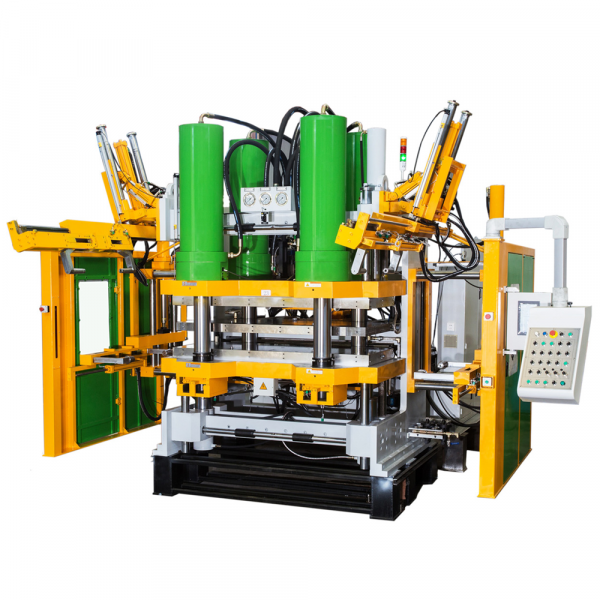
When your production line needs consistent splices, predictable cure and fewer reworks, the machine choices matter — and that’s where the practical physics of vulcanization kinetics meets daily shop-floor demands. Manufacturers working on heavy conveyor belts and deep-section seals often specify a belt vulcanizing machine rubber belt vulcanizing machine up front to control cure time and clamping force precisely, because uneven thermal gradients ruin batches fast.
What really controls cure in thick-walled components
Vulcanization is a chemical process driven by heat and time, and thick cross-sections shift the balance. Two things dominate: heat transfer into the core (thermal gradient) and the rubber compound’s cure kinetics. If mold temperature is high at the surface but slow to reach the center, the outer layer overcures while the core undercures, producing weak spots. You need controlled mold temperature, predictable heat flux and a matching cure schedule to get uniform crosslink density.
How China C-frame systems address the problem
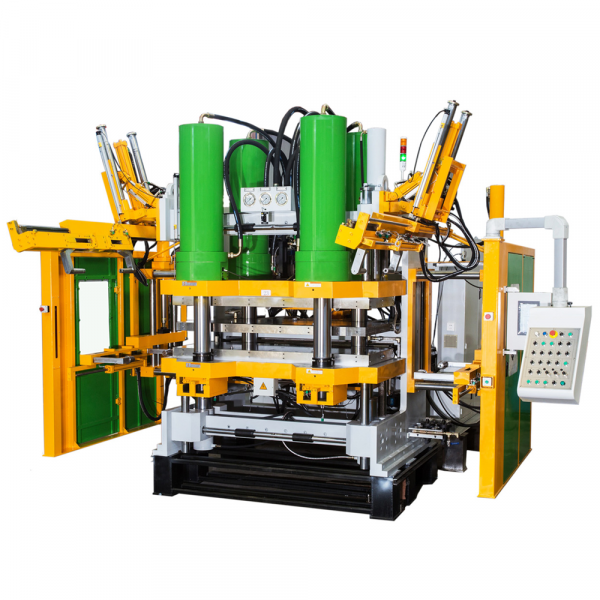
C-frame rubber injection machines used in many Chinese plants prioritize accessibility and fast clamp action while integrating multi-zone heating and thicker platen insulation. Operators adjust zone temperatures to reduce edge cooling, and they often pair this with longer, lower-temperature cycles to let heat penetrate without thermal shock. Add a correctly sized hot runner or balanced gating and you limit cold flow and air entrapment — little things that change cure profiles dramatically.
Real-world anchor: factory practice and results
At a conveyor belting facility in Dongguan, teams shifted from short, high-temperature cycles to multi-zone, staged heating after seeing a 12% scrap rate on 30–40 mm belt splices. Within weeks scrap dropped by nearly half; energy usage nudged down because they avoided repeated reworks. That practical change reflects documented lessons from global supply disruptions in 2020 — manufacturers had to stop guessing and control process windows tightly to keep output steady.
Common mistakes, practical fixes and alternatives
Typical errors are easy to spot: reliance on a single zone heater, underestimating cure time for thick sections, and neglecting compound-specific activation energy. Fixes are straightforward: profile the part with thermocouples, lengthen cycle modestly, and tune pressure so the rubber fills without squeezing out critical additives. Alternatives include using dedicated belt vulcanizing press setups for long splices, or employing preheating ovens to raise core temperature before mold closure — that reduces thermal gradient and shortens the effective cure window.
Design and process tips operators actually use
Keep the checklist simple. Match the rubber compound’s scorch and cure curves to your cycle. Use thermocouples at the core and near the surface during trials to map thermal gradient. Maintain consistent clamping force so flash control is repeatable. And document every slight setting change — small shifts in mold temperature or cure agent loading alter crosslink density and final mechanical properties.
Advisory — three metrics to evaluate systems and set specs
1) Temperature Uniformity Index: measure delta between surface and core at final cure — aim for the smallest workable spread for your compound. 2) Effective Cure Window: quantify how long the part spends within the compound’s optimal crosslinking range; prioritize processes that keep parts in that window rather than chasing short cycle times. 3) Yield per Energy Input: track scrap and rework against kWh consumed — a lower scrap rate with modest energy rise often wins economically. These three golden rules help you pick the right machine, tooling and schedule.
Final note — consistent processing and the right equipment solve most thick-part vulcanization headaches, and that’s where brands like HWAYI fit naturally: they build systems tuned for real shop-floor constraints and repeatability. —
