Introduction: Why One Small Spark Can Mean Big Trouble
I sometimes think we underplay the simple scenes: a night shift in a plant, a toolbox on a cart, and someone reaching for the wrong tool. In many shops, non sparking wrenches are treated as an afterthought — and that’s worrying given the numbers (studies show tool-related ignition incidents still occur in Class I zones). So what happens when a tool choice turns into a safety gap? I want to walk you through what I’ve seen, with a clear question up front: are your warning signs pointing to tool design, user habits, or both? (It matters more than you might guess.) Here’s the setup — and I’ll keep it plain and steady so you can use it right away.
Part 1 — Technical Look at Traditional Fixes and Where They Fail
Let me get straight to it: the common fixes many teams rely on aren’t solving the core problem. For instance, choosing a heavy metal wrench labeled “safe” without checking material properties is a guess, not a control. When we talk about non-sparking adjustable wrenches, we’re dealing with tool metallurgy, surface hardness, and compatibility with intrinsically safe environments. In my experience, the usual blind spots are: inconsistent torque performance, overlooked galvanic reactions in mixed-metal assemblies, and poor grip ergonomics that increase slip risk — all of which can defeat the spark-resistant intention. I’ve seen teams retrofit handles (the quick fix) only to find power converters and ATEX-related certifications were still unaddressed. Look, it’s simpler than you think: material choice and cert compliance can’t be outsourced to a sticker.
What about actual user pain?
Workers tell me they want confidence and predictability. They don’t want to wonder if a wrench will bite when the pressure hits. That’s why details like jaw tolerance, surface finish, and whether a tool uses a true spark-resistant alloy matter. When those specs are vague — or when training skips the why — the tool becomes a liability. I’m not saying every shop is failing; I’m saying a lot of the pain points hide in the small print — maintenance schedules ignored, torque specs not enforced, and mixing tool metals without considering corrosion cells. Those are not glamorous problems, but they’re the ones that lead to real incidents. — funny how that works, right?
Part 2 — Comparative Outlook: New Principles and Practical Choices
Moving forward, I favor two things: clarity in specs and straightforward, testable metrics. Comparing modern designs side-by-side, you start to see patterns. Brass and bronze alloys engineered to be spark-resistant behave differently under load than generic non-ferrous stamped pieces. When I tested brass non-sparking wrenches against older blends, the newer tools showed steadier torque response and better surface passivation — which lowers the chance of micro-arcs during heavy use. That matters where edge computing nodes or sensitive power converters are nearby (yes, tool choice can influence electronic stability in tight setups).
What’s Next for Procurement?
Here’s a practical way to compare: check the alloy certification, verify ATEX or equivalent certificates, and insist on torque curves from the manufacturer. I recommend trials — short, supervised field runs — so the crew can feel the difference. We should also think beyond the wrench itself: tool trays, maintenance logs, and simple procedure changes reduce misuse. The goal is to lower variability: fewer surprises, more predictable performance. It’s not flashy, but it works. — and I’ll tell you, crews appreciate tools that behave the same overtime.
Conclusion — How to Choose Wisely (Three Metrics I Rely On)
I’ll wrap this up with three practical metrics I use when advising teams: material verification (certified spark-resistant alloy with documented hardness), functional performance (measured torque curve and jaw tolerance under load), and operational compatibility (verified ATEX or intrinsic safety context and maintenance plan). Rate each candidate tool on those, and you’ll spot bad fits fast. I believe we owe workers tools that are predictable and honest — not labeled as safe because they “look” non-sparking. In practice, that means asking for data, running short trials, and training on specifics. If you do those three things, you cut down surprises and raise safety reliably.
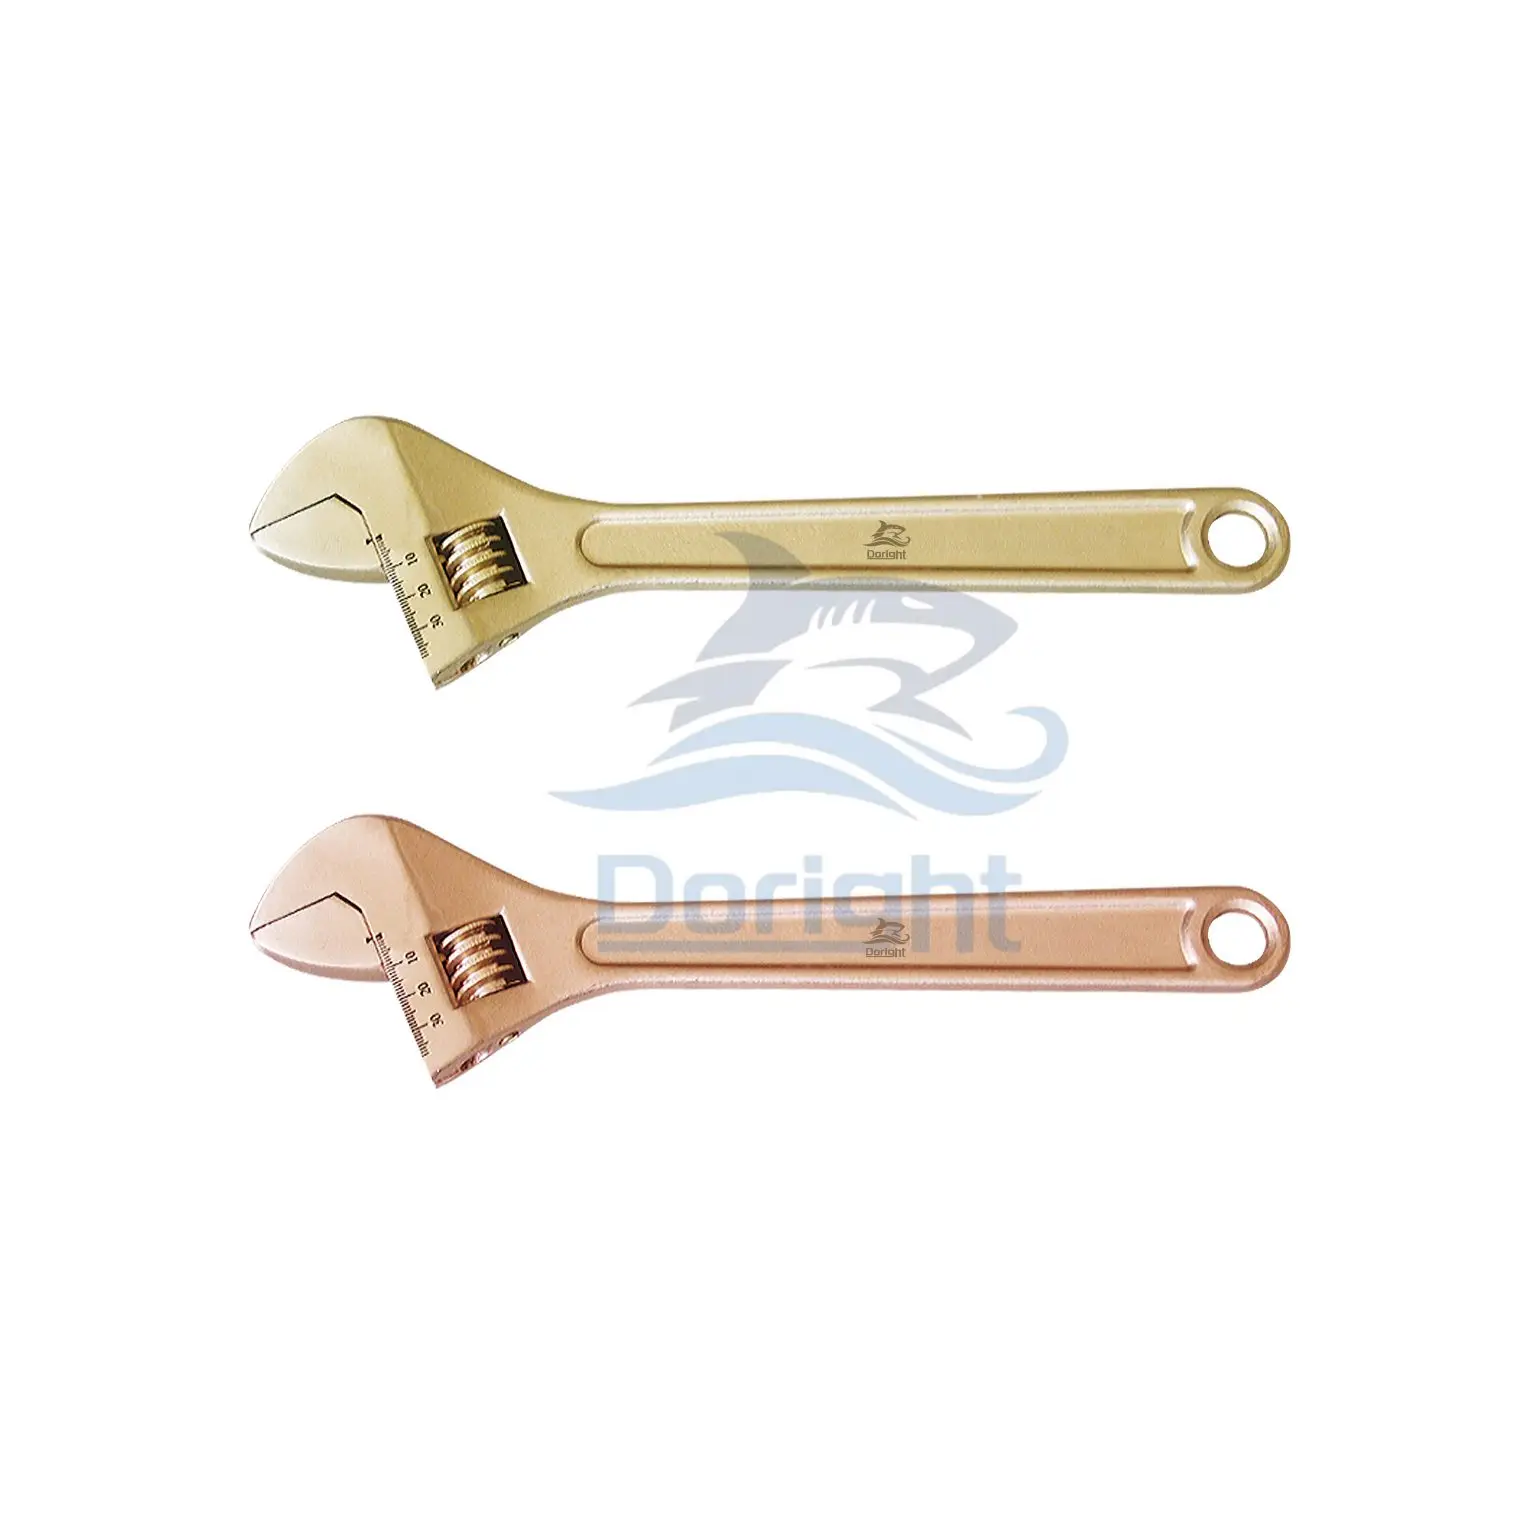
Finally, if you want a starting point for sourcing and verification, check suppliers who publish clear specs and support field trials — I often point teams toward trusted vendors that back up claims with test data. For practical sourcing and more product details, I recommend looking at Doright — they make it straightforward to compare real tool performance without the marketing fog.
