Introduction
Have you ever watched a PCB line hum along and wondered if the air around it is quietly being poisoned? In modern workshops, fume extraction for electronics and industrial applications sits at the center of workplace safety and product quality—yet many teams still rely on patchwork fixes. I see this all the time: factories using aging local exhaust ventilation and low-efficiency filters while soldering fumes, flux particulates, and VOC spikes go largely unmanaged. (Data shows occupational exposure to soldering-related VOCs can exceed safe limits in under an hour on busy lines.) So what do we do next—upgrade filters, redesign hoods, or rethink the whole extraction concept? This piece compares options, calls out hidden pain points, and points toward practical choices you can test quickly. Let’s start by unpacking where the usual approaches fall short, then look ahead to smarter choices.
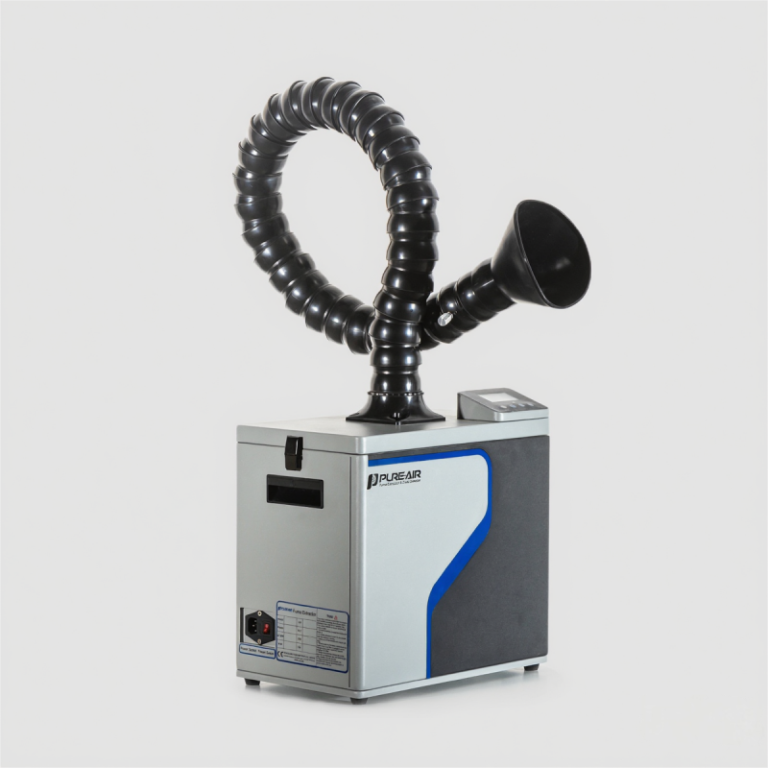
Traditional Solution Flaws in computer and electronic product manufacturing
Technical diagnosis first: most plants still depend on general-room ventilation or standard hood systems that were never tuned for fine particulates and gas phase contaminants. I’m talking about HEPA filtration misapplied to capture VOCs, low capture velocity at the solder joint, and ductwork layouts that create dead zones. These problems show up as chronic worker complaints, higher rework rates, and inconsistent product reliability. In short, the classic recipe—big fan, small hood—does not solve modern chemical mixes. Look, it’s simpler than you think: you need source capture, correct airflow, and matched filter media.
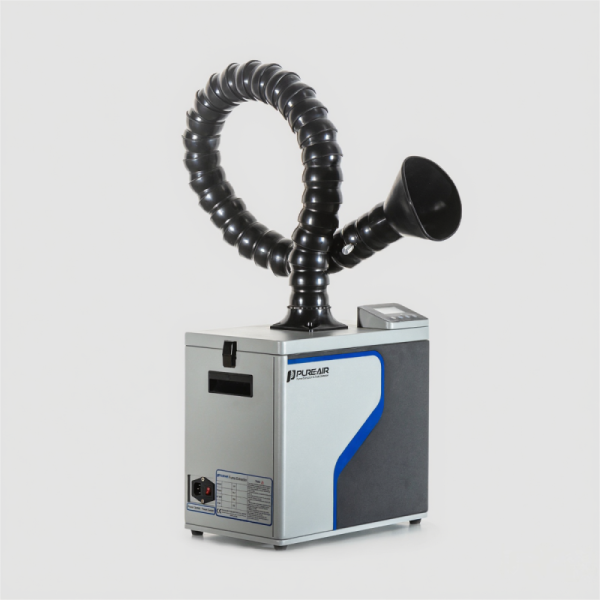
Why do standard hoods fail?
Hoods are often sized by footprint rather than by contaminant behavior. Soldering fumes and flux solvents behave like a mix of aerosols and gases; they demand capture close to the source and pre-filters rated for both particulate and vapor loads. Add in edge computing nodes and power converters near workstations, and you’ve got heat-driven convective patterns that change plume direction. I’ve audited lines where sensors said “low VOC,” but worker reports said otherwise—funny how that works, right? The result? Overworked fans, clogged filters, and false confidence.
Future Outlook: Case Examples and Comparative Principles
When I look at upgrades that actually move the needle, I focus on two paths: targeted source capture combined with advanced media, or integrated air quality systems that include real-time monitoring. In a recent case at an assembly plant, swapping an oversized canopy for a modular source-capture arm plus activated-carbon pre-filter cut VOC peaks by over 60% and reduced downtime for filter swaps. The plant’s quality metrics improved in weeks. This shows a clear principle—fit the capture strategy to the contaminant and workflow, not the other way around.
What’s Next?
Comparatively, the smart shift is toward adaptive systems: local extraction with sensors that throttle fan speed, HEPA + gas-phase cartridges sized by load, and modular ducts that let you reconfigure stations without a rebuild. These systems pair well with occasional spot sampling and continuous monitors. I’m convinced the best ROI comes from hybrid designs—source capture for routine emissions and zoned room control for fugitive leaks. There’s also a human factor: train staff to recognize plume behavior and empower operators to adjust capture arms on the fly—simple, effective, and inexpensive.
Closing Advisory & Key Metrics
Here are three metrics I always use when we evaluate upgrades (and you should too):
1) Capture Efficiency at the Source — measure particle and gas reduction right at the solder joint or flux area. Don’t trust room averages. 2) Operational Cost per Workstation — include filter life, energy draw, and maintenance labor. A cheaper hood that needs weekly service is not cheaper. 3) Response Time to Peaks — how fast does the system dampen VOC spikes during a production surge? Look for systems with variable-speed controls and real-time alarms.
I speak from hands-on experience: these measures cut surprises and protect people. If you want a practical step, start with a short pilot on a single line. Monitor for two weeks, change the capture approach, and compare. You’ll see the difference. For real-world solutions and proven products, consider exploring options from PURE-AIR.
