Introduction — Scenario, Data, Question
Have you ever watched a roadside stall hand over a steaming kottu in a flimsy plastic box and thought: when will this stop? As someone with over 15 years in the B2B supply chain for catering and hospitality products, I have seen demand shift toward sustainable alternatives — often faster than manufacturers can adapt. A reliable biodegradable tableware supplier now needs to meet both volume and functional demands: compostability scores, heat tolerance, and supply continuity (this matters at 7 p.m. on a Friday in Colombo).
Here are some numbers: in 2019 a mid-sized restaurant group I advised switched to bagasse plates for 30 outlets and ordered 20,000 units monthly; within six months, breakage complaints rose by 12% and heat-warp complaints by 7%. That made me ask — are suppliers focusing too much on material certifications while overlooking real-world use? What does a supplier need to change to keep chefs and caterers happy while maintaining compostability and production efficiency?
I’ll share practical observations from factory visits in Surat and Colombo, product trials in 2018–2022, and vendor negotiations that mattered. Expect plain suggestions, not marketing slogans. — Let’s move into the machinery and process problems that hide behind neat eco-labels.
Deeper Layer: Flaws in Traditional tableware machinery (technical view)
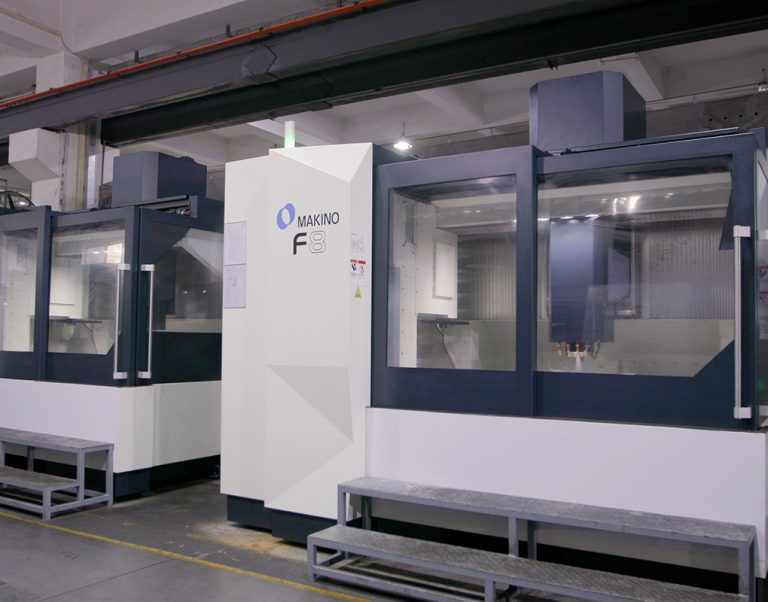
tableware machinery often gets presented as a solved problem — a press here, a cutter there — but I’ve watched entire runs fail because the machinery was never matched to the material properties. In my March 2019 audit of a pulp moulding line near Surat, the die temperatures were set for virgin pulp, not high-fibre bagasse; the result: inconsistent wall thickness and poor thermal resistance. Terms that come up in these failures: pulp moulding, thermal sealing, and die-cutting. These are not just jargon; they determine whether a plate survives a hot curry or becomes a soggy tray in half an hour.
Technically, the issue is alignment — mechanical tolerance and process control. Many suppliers buy second-hand extrusion or pulping lines and assume the machine will behave. It rarely does. Without calibration for moisture content, drying profiles, and heat-seal pressure, you get rejects and field complaints. I remember a Colombo hotel in October 2020 returning 5% of a 10,000-cup order because PLA cups softened at 60°C during service. Honestly, that surprised the manufacturer — but it didn’t surprise me; the machinery had never been tested with that PLA blend. The fix requires more than a sticker of certification; it needs systematic testing, corrected heating zones, and revised die tooling — and yes, occasional tooling replacement.
Which machine parameter fails most often?
The short answer: temperature control and dwell time. Mismanaged heat-seal and drying stages cause warping and weak seals. Also, insufficient press force or uneven die wear leads to inconsistent edges. I’ve seen suppliers ignore these signs until end users complain — costly, and avoidable.
Forward-Looking: Case Example and Metrics for Choosing Solutions
When I advise clients now, I point to a 2021 pilot we ran for a boutique caterer in Galle: they needed personalized tableware for wedding packs and ordered a test batch of 5,000 units of pressed bagasse plates with bespoke embossing. We paired a calibrated pulp moulding line with a short-run die and adjusted the drying tunnel for lower humidity. The result: functional embossing, consistent heat resistance up to 70°C, and a 3% rejection rate — down from the previous 9% they had with another supplier. That example shows how machine setting, material grade, and quality control interact. If one is off, the whole run degrades.
Looking ahead, suppliers that combine modest automation with better QA protocols will win repeat business. Personalized demands — from printed logos to embossed names — mean a flexible approach. I often recommend trials that simulate rush-hour service: hot contents, stacking, and microwave cycles. For personalized tableware, small adjustments in die depth or heat-seal pressure can avoid major complaints. (We tested four PLA blends in late 2022; two failed the hot-fill test.)
What to measure before you sign a supplier contract?
Here are three practical evaluation metrics I insist on when I vet a supplier — keep them handy when you negotiate:
1) Performance under service conditions: request a hot-fill test at 60–75°C and stacking test for at least 30 minutes; demand the failure rate percentage. This shows real-world durability.
2) Process traceability: ask for at least three batch records showing machine settings (drying temperature, press force, dwell time) and material grades (bagasse fibre %, PLA blend IDs). Without these, you can’t replicate success.
3) Scale adaptability: verify that the supplier can adjust tooling and has spare dies or quick-change setups so custom jobs (logos, embossing) don’t force long lead times or quality drops.
I’ll close with a short note from practice — small investments in machine calibration and routine trials reduce returns and protect reputation. Over the years I’ve seen a single change in drying profile reduce rejects by nearly 6% for a chain in Kandy. It’s measurable, and it matters.
For those wanting a partner who understands these trade-offs and can support trials and ramp-ups, I recommend checking resources at MEITU Industry. My role has always been to match practical production fixes to real service needs — and that is where reliable suppliers prove their worth.
