Introduction — a shop-floor morning
I still remember the smell of cutting oil on a Monday morning, the tiny clink of a tool carousel snapping into place. The shop was warm; the machines humming like kettles. CNC turn mill center manufacturers line up choices every day, and they do so under a stack of charts and urgent orders. Last quarter, a mid-sized shop I advise reported a 12% scrap rise after a rush to meet a big contract — numbers that sting when margins are thin. So I ask: how do we stop firefighting and build a workflow that actually holds steady under pressure? (There’s grit in the gears, literally.)
Picture a row of control panels, the glow of an HMI, and a machinist leaning over a screen. You can feel the pace. The data says downtime and rework cost far more than the newest spindle or tool turret. We need to face the immediate problem: production drift happens, and it costs time, confidence, and clients. I’ll walk through what I’ve seen fail, why it fails, and what to try next — step by step. Let’s move on to the core problems that hide under good-looking specs.
Part 2 — Why the usual fixes miss the mark
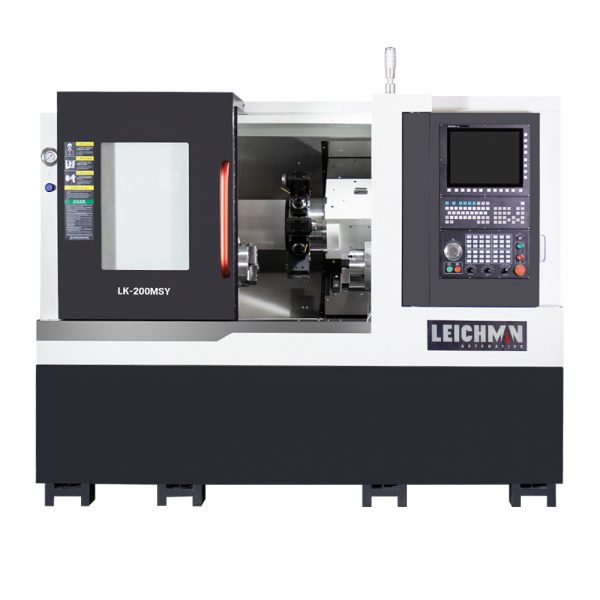
When shops say they upgraded to a cnc turning and milling center, they expect instant gains. I’ve watched that play out. Often, the machine is fantastic on paper: higher spindle speed, more axes, live tooling. Yet yield doesn’t jump. Why? The answer lives in the seams — the handoffs between setup, program, and operator. Tool offsets drift. G-code tweaks get patched in by memory, not revision control. Chip evacuation is overlooked until a jam stops a run. Look, it’s simpler than you think: a shiny machine doesn’t fix a messy process. — funny how that works, right?
We habitually blame the machine, not the mix of weak standards and spotty communication. I’ve seen tool turret indexing errors blamed on parts, when the root cause was a poor fixture or a misdocumented tool life. Axis synchronization problems show up as chatter or bad tolerances, but they often trace back to inconsistent clamping or worn bearings. In short: the traditional solution stack—buy, install, train—often skips the systems layer: standardized setups, versioned CNC programs, and a feedback loop for spindle load and cycle time. If you care about repeatable precision, start there. (I mean it.)
What specific pain do shops hide?
Small things: undocumented offsets, lax tool checks, ignored alarm histories. Big things: no single source of truth for process parameters, and no plan for gradual drift. These are the real culprits behind missed delivery dates and surges in scrap.
Part 3 — Principles for the next generation: a forward look
I want to sketch the tech and habits that actually help. First, connect measurement to action. Fit your cells with simple sensors for spindle load and coolant flow. Feed that data back to a local logger or MES. Second, enforce program control: stamp every G-code change with an author and reason. Third, standardize fixtures and clamping checks before each batch. These principles let the machine reach its potential without relying on heroic operators. I’ll note one more idea: modular fixturing reduces setup time and variation — it’s boring but effective.
Also, think about the machines you pick. A cnc vertical turning lathe can be the right choice when large diameters and heavy cuts are common. But it still needs the same disciplined process around tool life and chip control. In practice, marrying machine capability with tight process control drops scrap and builds trust with customers. Real-world: one shop reduced cycle variance by 35% after introducing simple cycle-time targets and a checklist for tooling. — but that’s just from my shop-floor view.
Closing — three metrics I use when choosing solutions
I’ll end with practical criteria you can use tomorrow. When I evaluate a vendor, a machine, or a shop plan, I ask three clear questions: 1) Can I measure it? (If not, I can’t manage it.) Track spindle load, cycle time, and tool life. 2) Can I repeat it? (Check fixturing, program control, and operator steps.) 3) Can I recover from drift? (Look for alarm histories, quick-change tooling, and easy calibration.) These metrics are simple. They force action. They also make ROI visible in weeks, not months.
I’ve said enough to get you started. I care about real, usable improvements more than glossy specs. If you want a partner that focuses on these practical changes, look at the tools and support offered by Leichman. I’ll be candid: the machines alone won’t save you. The process will.
