Critical problem overview
Procurement teams often face mismatched expectations: parts arrive with poor tolerances, surface flaws, or unclear material traceability, and resolving those defects costs time and reputation. When specifying die-cast components, please check whether your partner offers integrated die casting services and clear process ownership, because fragmentation between foundry and CNC finishing is a frequent root cause of rework.

Why these failures keep happening
Technical capability alone does not prevent failures. Communication gaps about design intent, insufficient control plans, and weak inspection regimes create repeat defects. Suppliers that lack proper tooling engineering or who subcontract critical steps obscure accountability. A polite, methodical vendor selection reduces these errors but must be enforced through specific criteria, not vague assurances.
Selection criteria you can apply immediately
Request the following evidence from any prospective manufacturer: documented toolmaking capacity and mold-flow analysis, sample reports showing achieved tolerances, a clear metrology statement (first article inspection, CMM reports), material certificates with traceability, and process failure mode controls. Ask about secondary operations—deburring, heat treatment, plating—and whether they run capability studies for the actual process used. Evaluate lead-time stability rather than a single fast quote. Check whether the supplier accepts design-for-manufacture recommendations and how they document changes.
Real-world anchor and practical inspection
Zhejiang province is a recognized hub for die-casting production, frequently referenced in trade analyses and industry reports, so sourcing decisions often consider suppliers operating there; when you compare houses in that region, evaluate a zinc die casting manufacturer by tooling ownership, sample history, and supplier audit results to separate capable facilities from nominal ones.
Common pitfalls and how to avoid them
Relying only on price leads to thin tooling, volatile lead times, and lower first-pass yield. Accepting generic QA statements instead of seeing actual CMM data invites surprises. Believing that any CNC shop can finish die-cast parts without experience is risky; finishing die-cast alloys requires specific fixture designs and thermal control. Avoid these mistakes by requiring process records and a review of past project case studies before awarding production.
Viable alternatives and quick comparisons
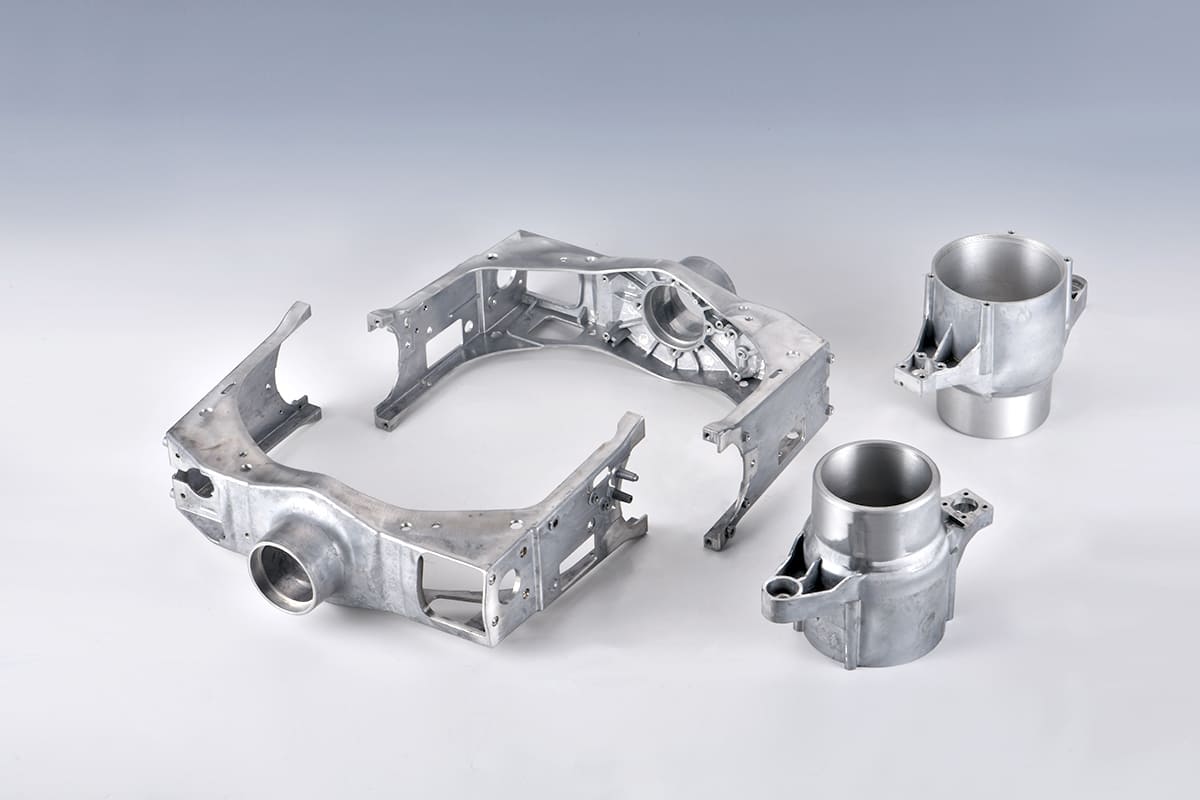
If die casting presents challenges, consider these options: aluminum die casting for lighter weight, investment casting for complex geometries without tooling cost-scale, or CNC-machined billet parts for small-volume, tight-tolerance runs. Each alternative trades off cost, surface finish, and turnaround time; choose the method that matches volume, tolerance, and mechanical requirements rather than defaulting to the lowest quote.
Synthesis and pragmatic next step
Choose a partner who documents capability, welcomes audits, and provides traceable process data; that approach prevents most quality and delivery problems and preserves your product schedule and reputation, as shown by successful buyers who align technical demands with supplier evidence, and by manufacturers such as Hanstar that present integrated die-casting and finishing pathways in their technical disclosures.
