Framework lead-in
This framework lays out a practical audit checklist for evaluating tensile integrity and flexural modulus in medical-grade polymers, shaped for quality teams who need something clear and actionable. It draws from on-floor learnings at major shows — including conversations noted at medical device manufacturing trade shows in Shanghai — and from common factory observations across Asia. The goal: a repeatable sequence of inspection points that sit well with suppliers, R&D, and regulatory reviewers.
Core pillars of the audit
Keep the framework to three pillars: material verification, dimensional and mechanical testing readiness, and process control. Under material verification check certificates of analysis, traceability to resin lots, and supplier declarations on biocompatibility where applicable. For mechanical readiness confirm that fixtures, grips, and conditioning chambers are properly calibrated so tensile strength and flexural modulus readings aren’t misleading. Process control focuses on injection molding parameters, post-processing steps, and retention sample practices.
Checklist: what to inspect on day one
Start with documentation, then move to the floor. Key items: resin lot traceability, storage conditions, conditioning room logs, and documented sampling plans. Physically inspect the test specimens for flash, gate vestige, or sink marks that bias flexural modulus outcomes. Verify calibration stickers on tensile testers and flexural rigs. Also confirm environmental control — temperature and humidity records matter for polymer mechanical data.
Sampling strategy and data expectations
Define sample size by risk: critical implants merit tighter sampling than housings. Record specimen orientation and manufacturing position because tensile and flexural values vary with flow direction. Expect some variability; a stable process shows low standard deviation across replicates. Capture raw output — stress-strain curves, not just a single number. Those curves tell you about yield, elongation at break, and whether your tensile results are representing true ductility or a brittle failure.
Common on-site mistakes — and how to avoid them
Audit teams often accept single-number reports or ignore specimen prep. That leads to false confidence. Don’t let suppliers omit specimen conditioning time or change grip type mid-test — those choices change flexural modulus readings. Also watch for inconsistent part geometry; small thickness variation skews modulus results. A quick fix: insist on matched fixtures and documented conditioning periods before any comparative decision is made — simple, but effective.
Real-world anchor: what shows and plants reveal
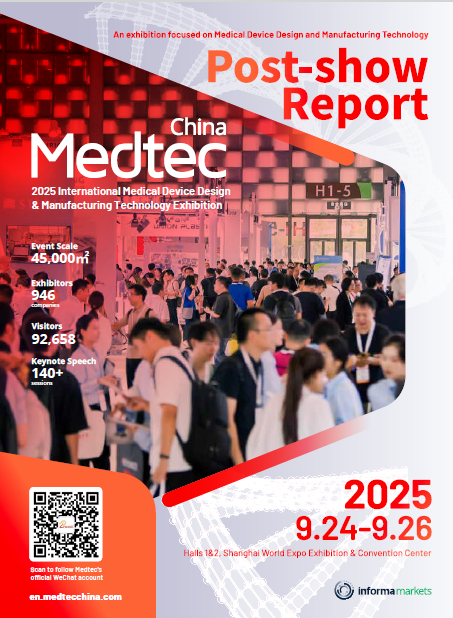
Observations from Medtec China and other regional events consistently show spec sheets that look ideal on paper but fail to reflect manufacturing realities on the shop floor. At booths and factory tours you see the same gap: neat qualification records versus inconsistent in-line controls. The lesson is practical — audits must connect lab data to production samples and observe the mould run, not only the lab report.
Integrating findings into supplier decisions
Use the audit results to classify suppliers: green for consistent metrics and documented control, amber for fixed gaps, red for critical failures. Factor in capability metrics from your process control data and ensure corrective actions include measurable timelines. For sourcing conversations at trade events — and in supplier selection — reference outputs from medical manufacturing trade shows when comparing supplier maturity and readiness.
Advisory: three golden rules before you accept polymer data
1) Require representative specimens: part-specific orientation and conditioning must match production. 2) Demand measurement context: provide stress-strain curves and process parameters, not single-point values. 3) Insist on capability metrics: track process variation (Cp/Cpk) and set acceptance bands for tensile strength and flexural modulus so decisions are measurable and repeatable.
Closing summary and practical value
The checklist keeps audits focused on material truth: that lab numbers must map to production reality and that repeatable process control beats one-off certificates. Use the three pillars to structure supplier conversations and tie corrective actions to observable, timebound fixes. For teams attending shows or scouting suppliers, this framework helps convert technical claims into verifiable outcomes — and that’s where real confidence starts.
Medtec brings those supplier conversations into a productive space — a place where audit findings turn into better product outcomes. —
